Industry Overview
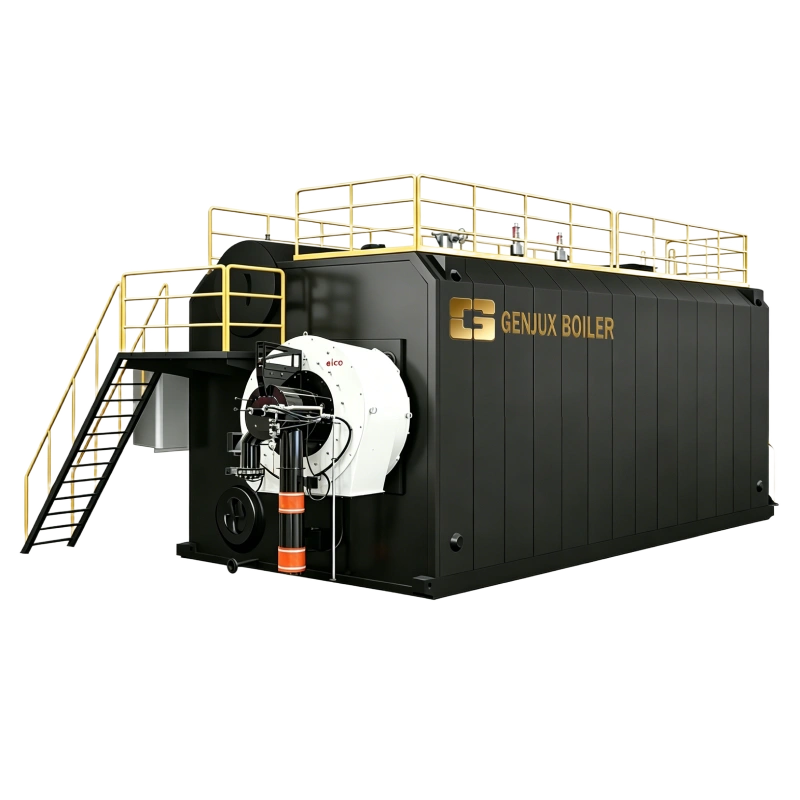
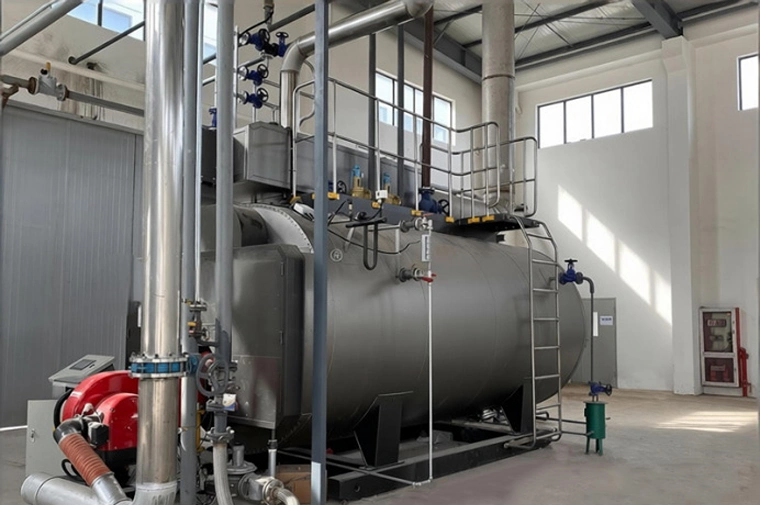
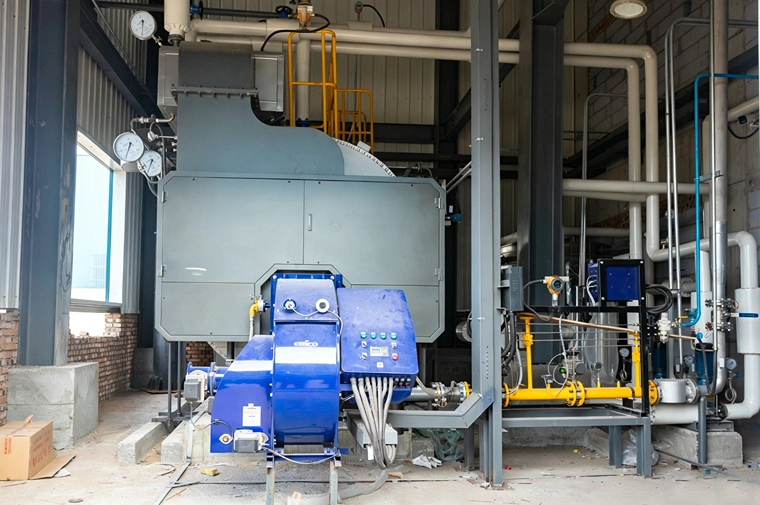
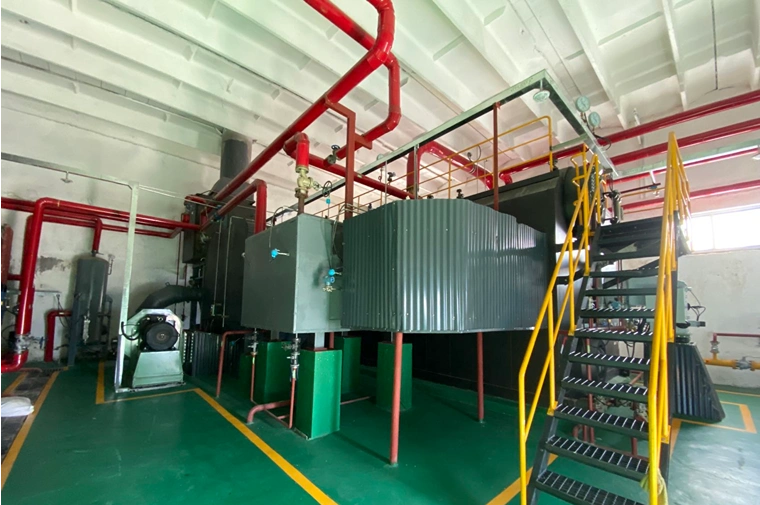
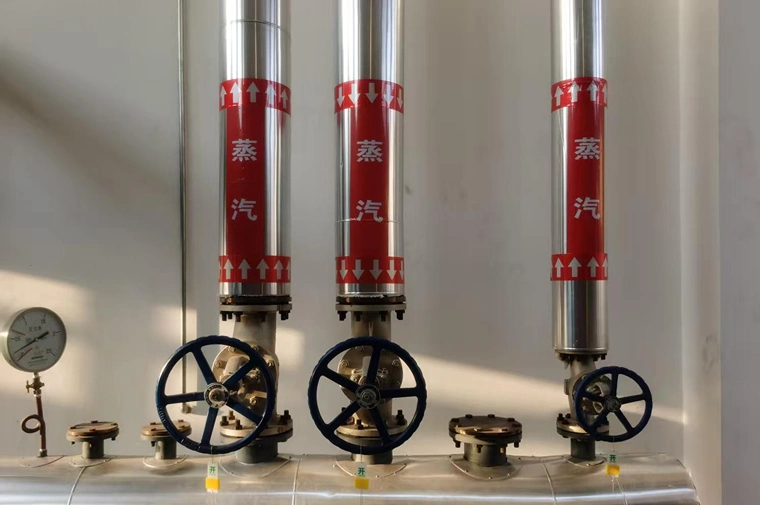
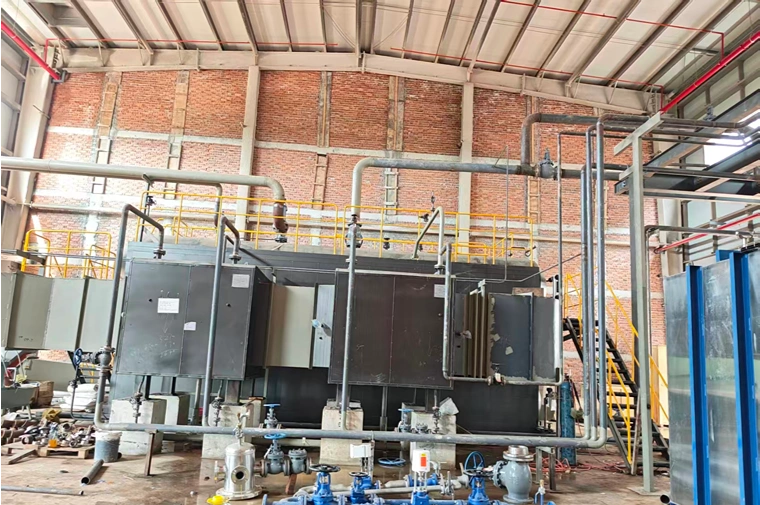
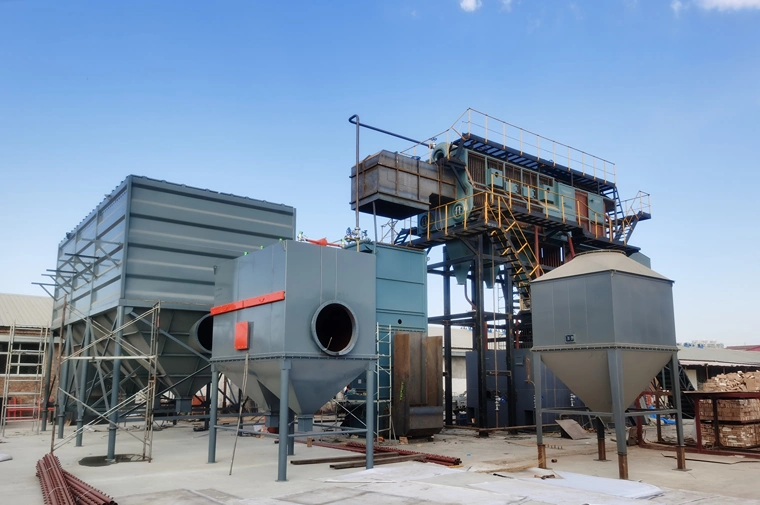
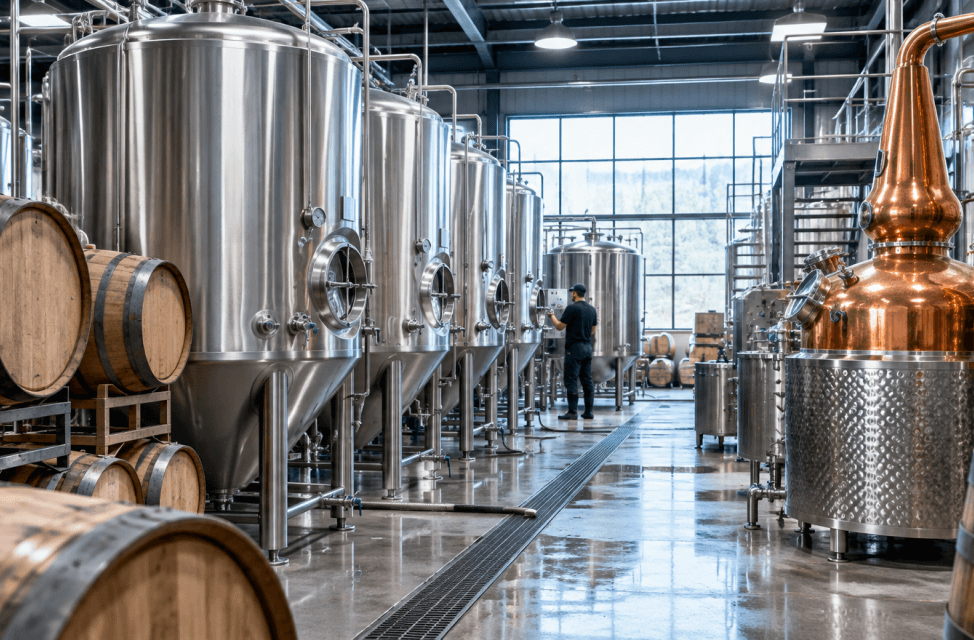
The chemical industry covers a wide range of products, mainly involving processes such as reactor heating, raw material distillation and constant-temperature reactions. Temperature and pressure requirements vary greatly across different processes. Genjux Boilers has extensive project references and rich experience serving the chemical sector, helping chemical enterprises stabilize process control and cut operating costs.
Industry Pain Points
Reaction temperatures must remain constant over long periods. Temperature fluctuations lead to incomplete reactions and increased by-products.
Explosion-proof requirements apply to some production sites.
Chemical parks enforce systematic management on equipment safety, emissions and operational monitoring.
Solutions
Recommended Boiler Selection:
| Coal-fired Chain Boiler | Coal-fired Fluidized Bed Boiler | Biomass Boiler | Gas Boiler | |
| Equipment Investment | Medium | Relatively Large | Medium | Relatively Low |
| Steam Cost | Relatively Low | Lowest | Medium | Relatively High |
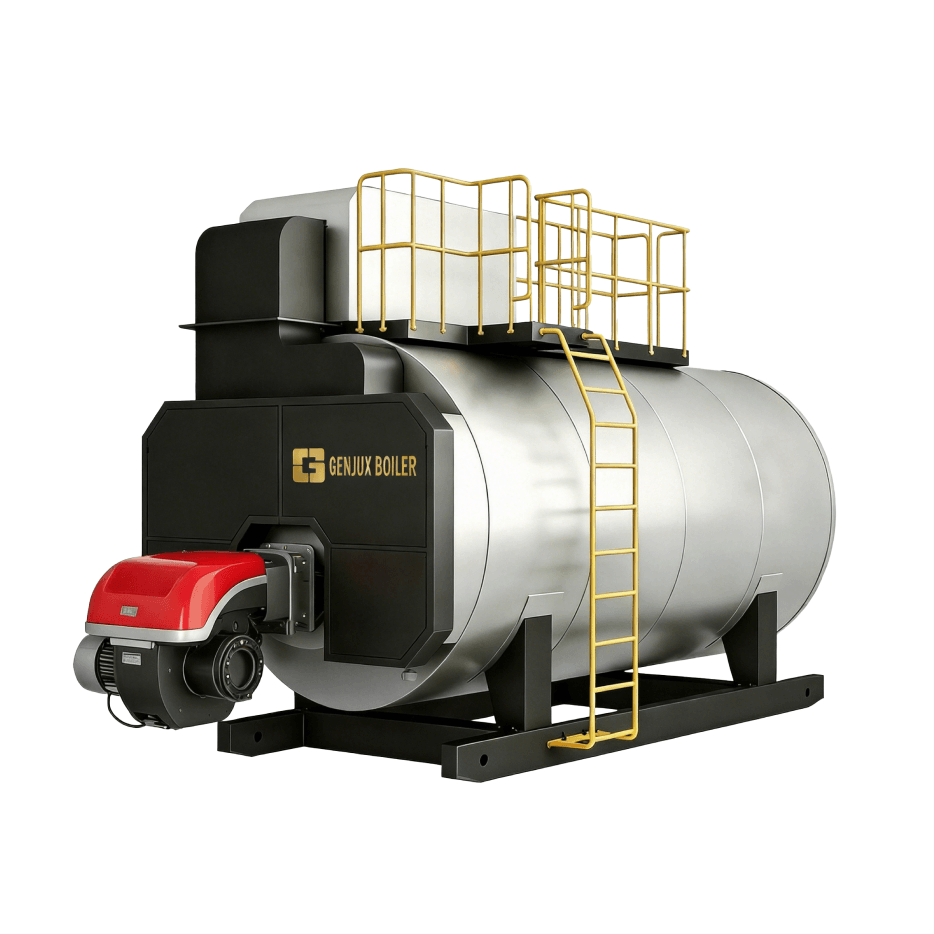
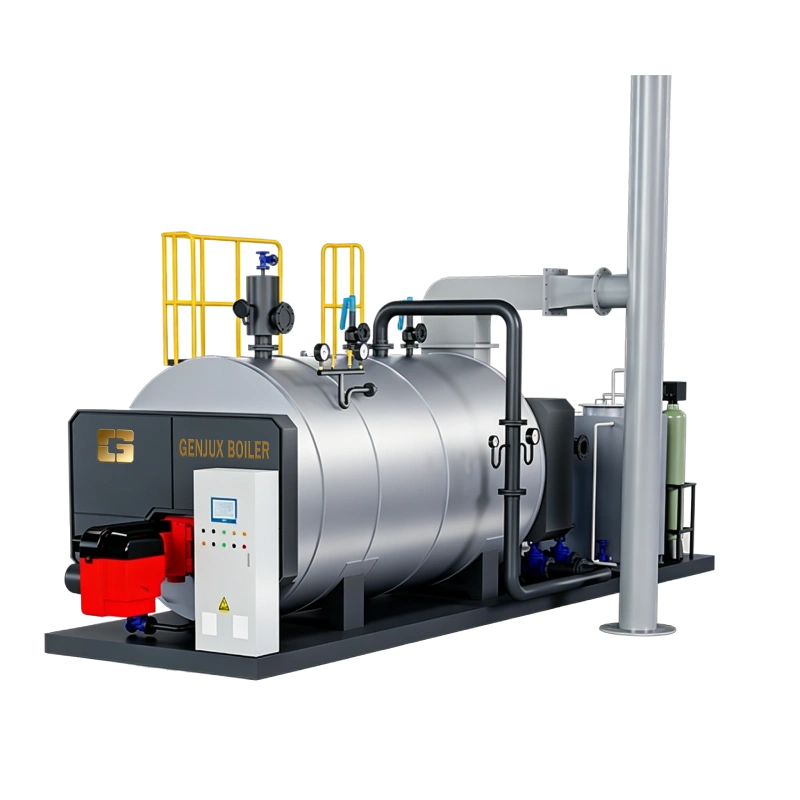
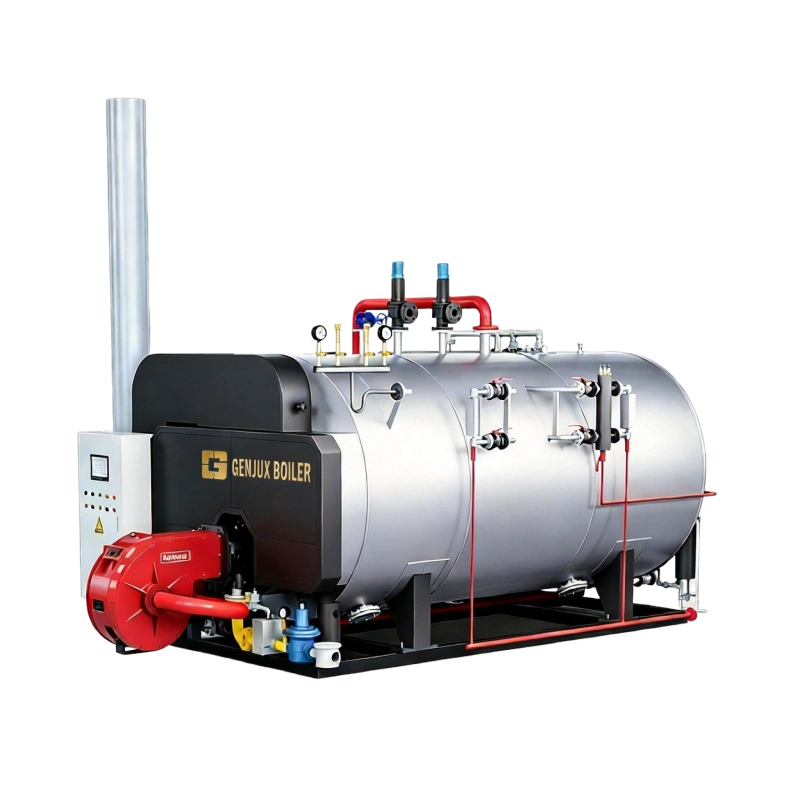
Select either a steam boiler or thermal oil heater according to the process temperature requirements of the medium.
Core Values
Explosion-proof & safe operation
Continuous and stable heat supply
Low-NOₓ emissions
Keywords
Explosion-proof
Continuous Heat Supply
Low-NOₓ Emissions
Thermal Oil Heater
Palm oil
Biodiesel
Refining
Petrochemicals